A wind turbine builder needed six main shafts with full traceability from the melt, tested to its own ultrasonic acceptance class.
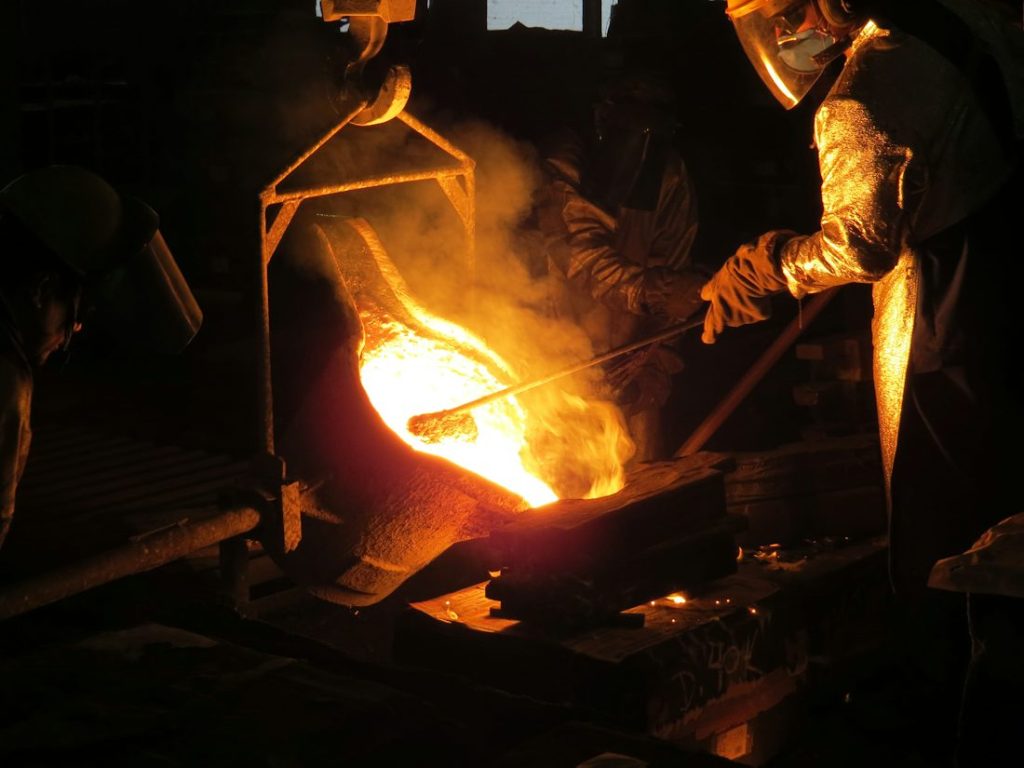
We poured 34CrNiMo6 ingots, forged the shafts on the 2,500 t press with the reduction recorded for every piece, then quenched, tempered and rough machined them before ultrasonic testing.
02What we did
Melt to machined shaft on one site
Poured the 34CrNiMo6 ingots in our own melt shop
Forged each shaft with the reduction ratio and temperatures on record
Quenched and tempered, then rough machined to the customer drawing
Ultrasonically tested every shaft to the customer's acceptance class
12wksFrom order to dispatch
6MWTurbine rating
6shaftsForged, tested and delivered
“Traceability from the ladle to the finished shaft is what our certifier asked for. We got it in one dossier.”