02Service
Open-dieforging.
Shafts, rings and blocks up to 18 t
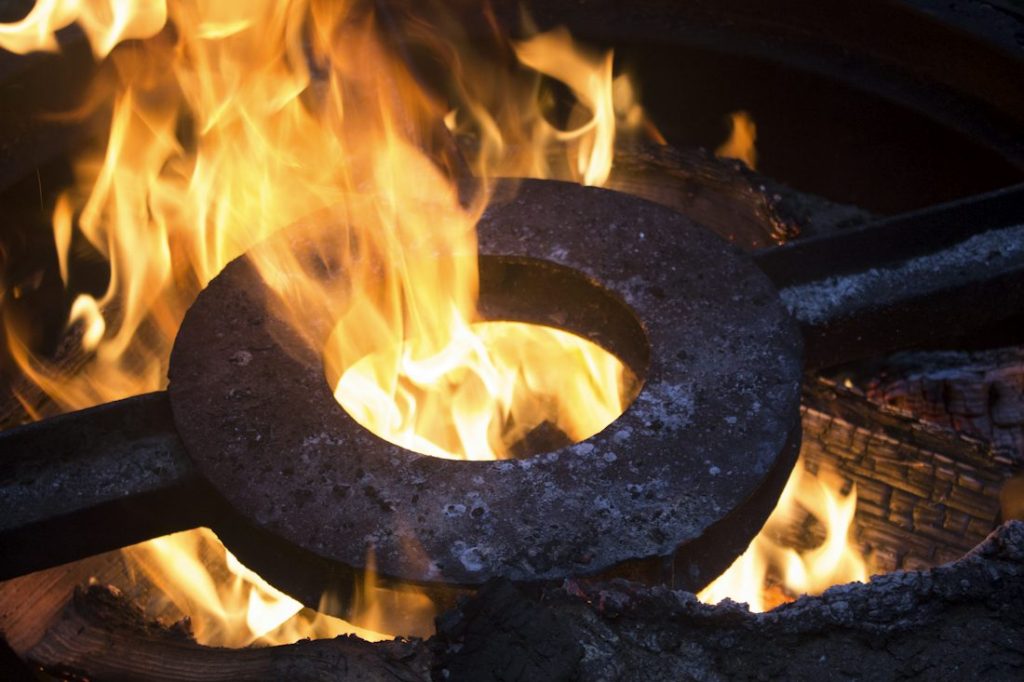
Shafts, rings, discs and blocks up to 18 t, forged on a 2,500 t press from ingots we melt ourselves.
Because the ingot is poured in our own melt shop, the heat number, chemistry and cleanliness data carry straight through to the forging. Reduction ratios and forging temperatures are logged for every piece.
Most forgings leave rough or finish machined, heat treated and ultrasonically tested, with one certificate covering the whole route.
Next service
Heat treatment
Quench and temper, normalising, stress relief and case hardening in furnaces surveyed to AMS 2750.