Steel ring heating in a furnace

03Service

Heattreatment.
Molten steel glowing in a furnace mouth

Twelve furnaces, one calibrated record

Quench and temper, normalising, annealing, stress relief and case hardening in twelve furnaces surveyed to AMS 2750.

Gas and electric furnaces up to 6 m long cover everything from a single flange to a 25 t shaft. Every load is logged with thermocouple positions, times and temperatures, and the chart ships with the parts.

We heat treat parts made elsewhere too, with exactly the same records and the same lab testing.
Max. temperature1,150 °C
Furnace lengthup to 6 m
Max. load25 t
Quench mediaWater, polymer, oil
SurveysAMS 2750 class 2
Records kept10 years

Calibrated traces

Every load ships with the furnace chart, thermocouple positions and times.

Tempered to target

We temper to the hardness window you need, then prove it on the part.

Your parts too

Heat treatment for parts made elsewhere, with the same records and testing.

Steel coils in a warehouse
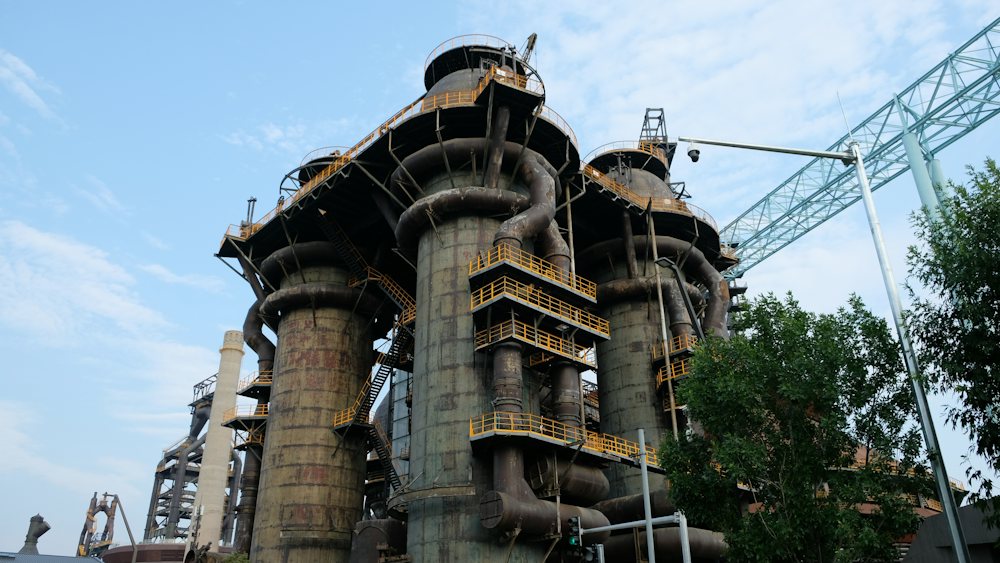
Blast furnaces with yellow stairways

Questions about heat treatment

Yes, with the same records. Send the grade, required properties and part weight.

Stress relief is usually 48 hours. Quench and temper with testing takes five to seven working days.

Customer and third-party witnessing is welcome. Book at least three working days ahead.

Next service

CNC machining

5-axis milling and turning up to 4 m, with CMM inspection before anything is packed.
Buy Theme - $49 Launch It For Me