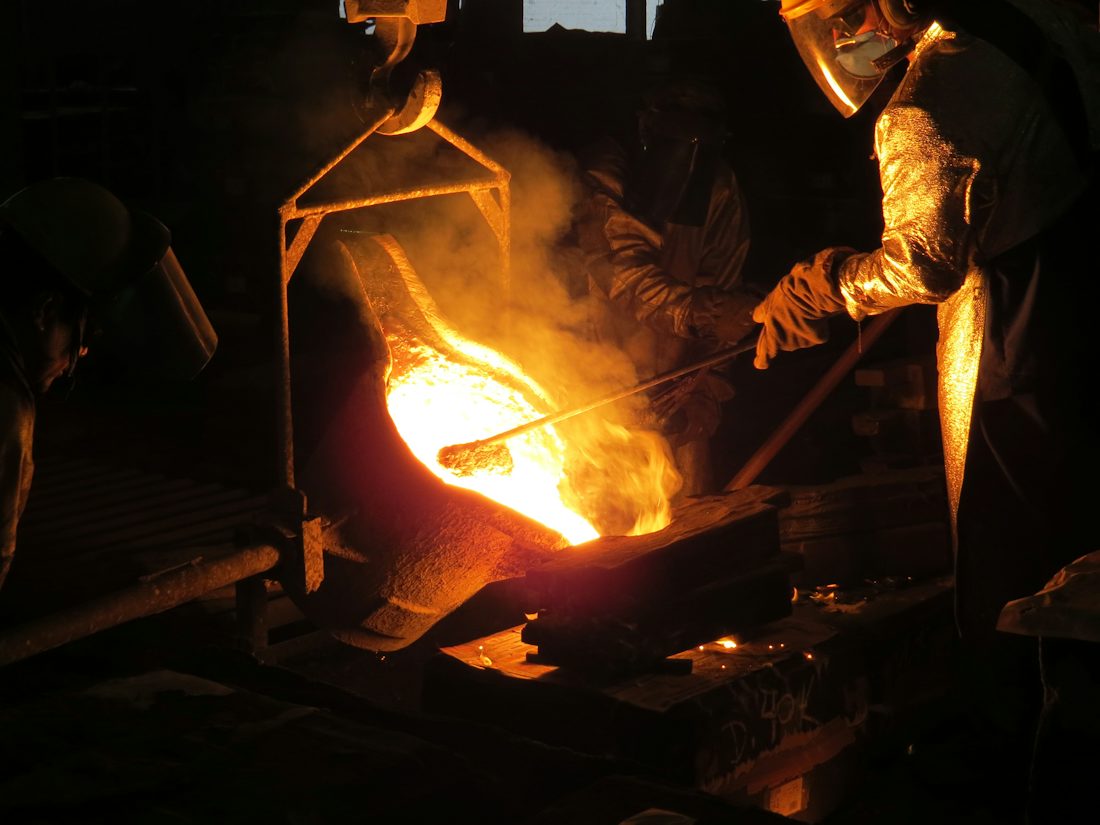
Smith holding glowing iron with tongs

02Service

Open-dieforging.
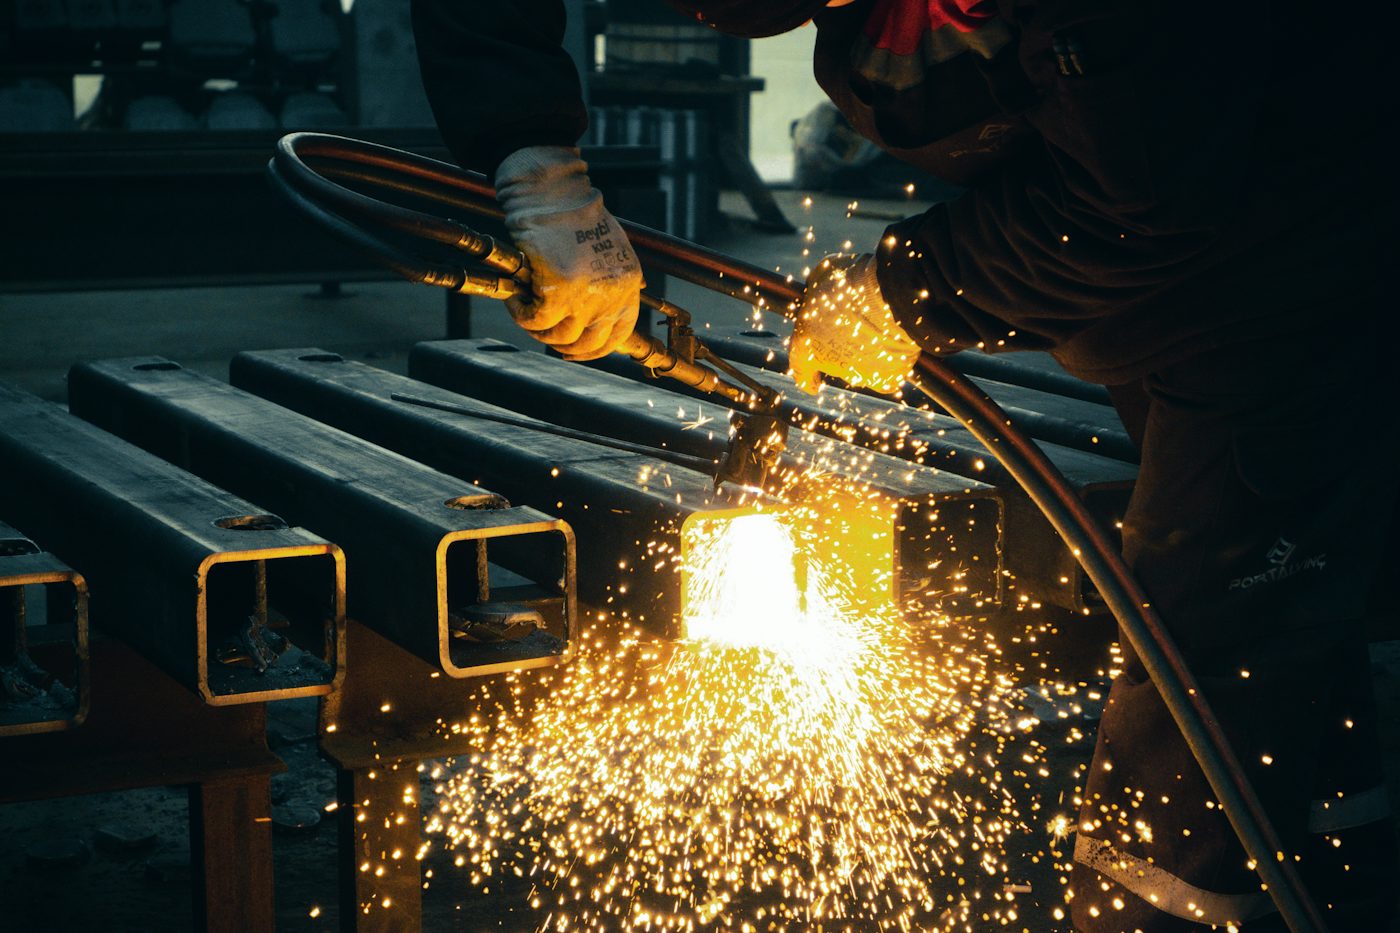
Sparks flying off steel sections

Shafts, rings and blocks up to 18 t

Shafts, rings, discs and blocks up to 18 t, forged on a 2,500 t press from ingots we melt ourselves.

Because the ingot is poured in our own melt shop, the heat number, chemistry and cleanliness data carry straight through to the forging. Reduction ratios and forging temperatures are logged for every piece.

Most forgings leave rough or finish machined, heat treated and ultrasonically tested, with one certificate covering the whole route.
Max. piece weight18 t
Press2,500 t hydraulic
Shaft lengthup to 9 m
Ring diameterup to Ø 1,800 mm
Grades42CrMo4, 34CrNiMo6, S355
StandardEN 10250 / ASTM A668

Own ingots

Forgings start from ingots poured here, so the melt record carries through.

Reduction on record

Forging ratio and temperatures are logged for every heat and every piece.

UT before dispatch

Every forging is ultrasonically tested to EN 10228-3 before it ships.

Coiled rebar
Worker in a welding helmet grinding a steel beam with sparks

Questions about open-die forging

At least 3:1 on shafts and 4:1 where the standard or your drawing requires it, recorded per piece.

Yes. Most forgings leave rough or finish machined, heat treated and UT tested.

We prefer our own melt for traceability, but we can forge supplied material when it comes with its certificates.

Next service

Heat treatment

Quench and temper, normalising, stress relief and case hardening in furnaces surveyed to AMS 2750.
Buy Theme - $49 Launch It For Me