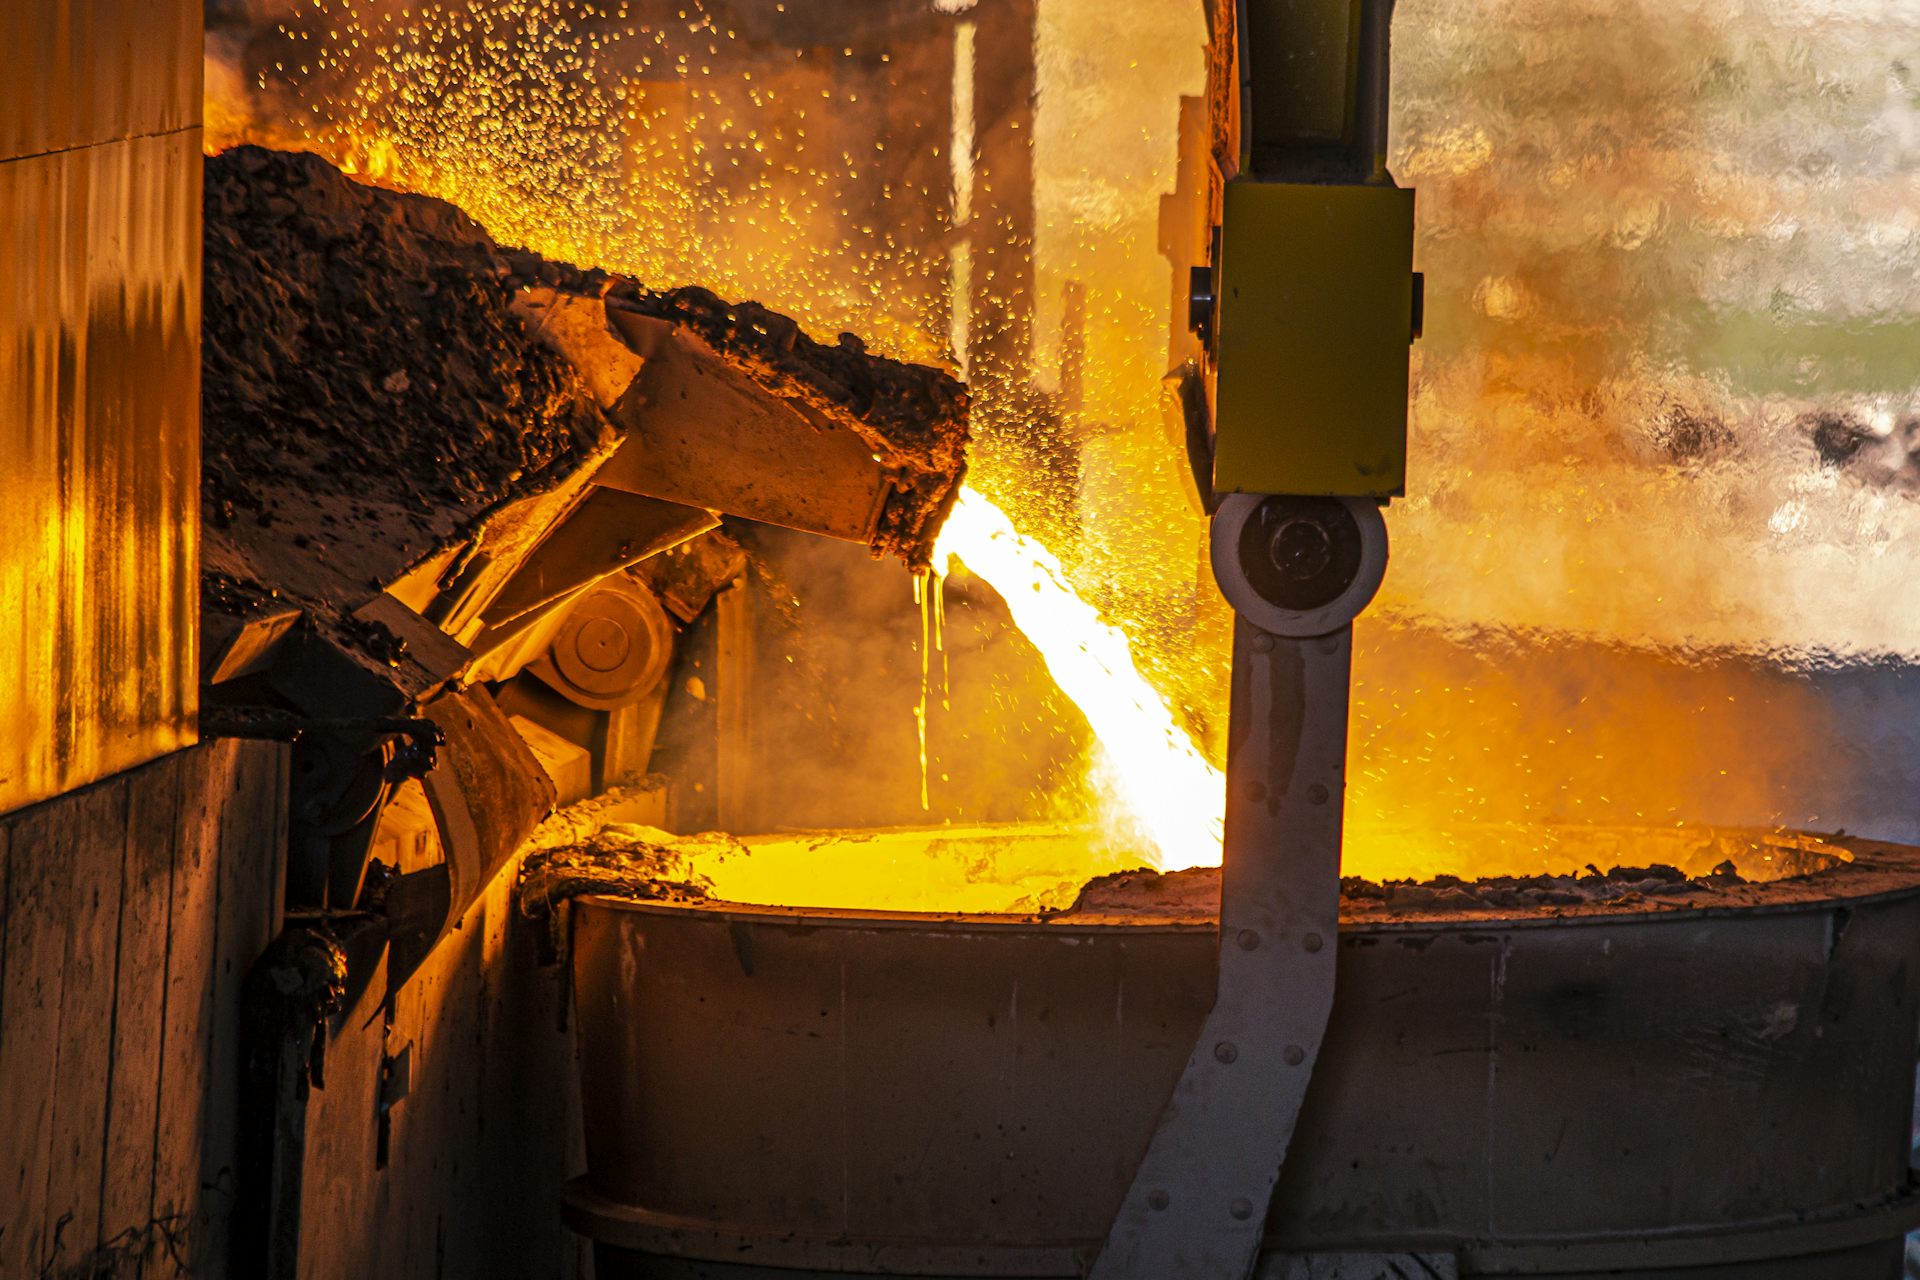
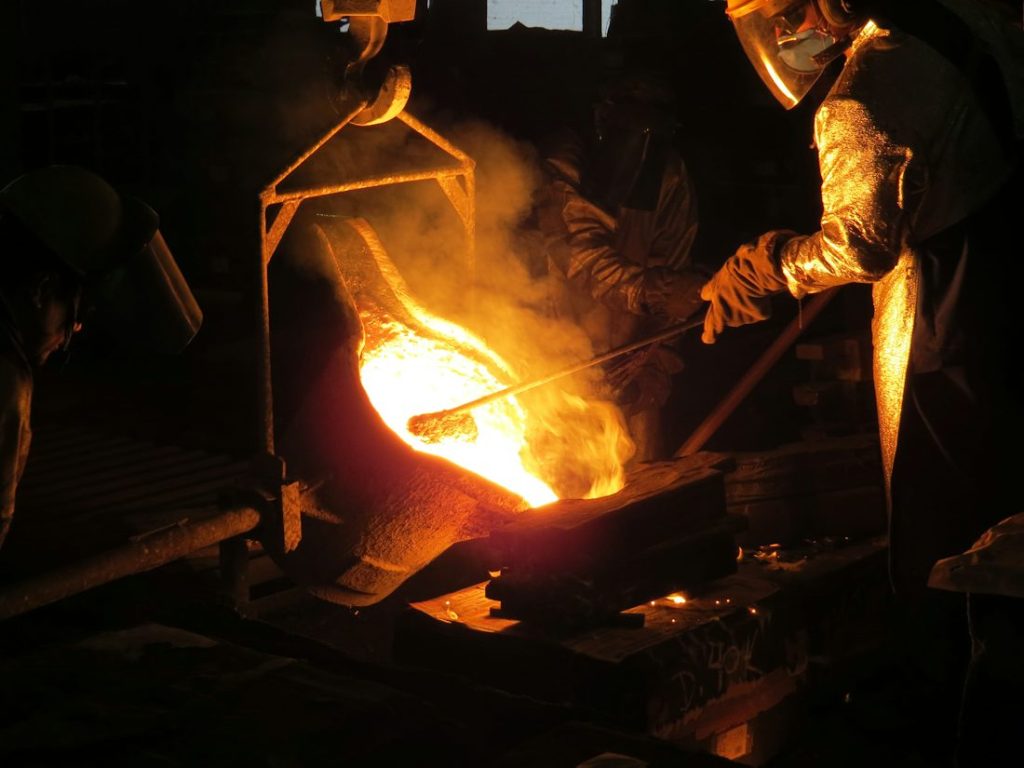
Molten metal pour

01Service

Melting &casting.
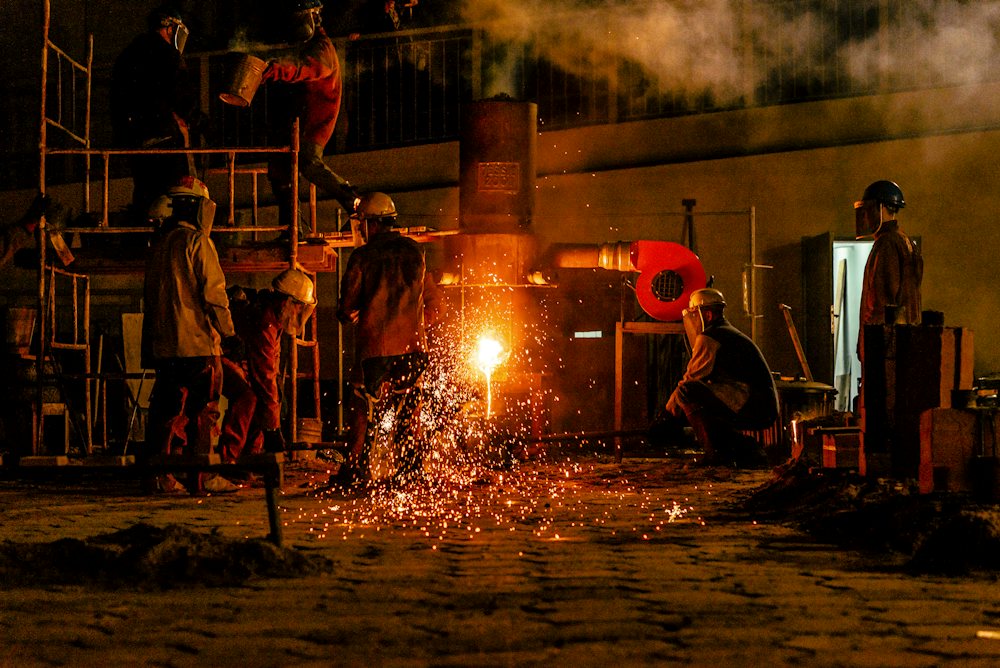
Foundry crew beside a stream of molten metal

Poured to specification, from 50 kg to 12 t

Induction melting from 50 kg to 12 t, poured into sand or investment moulds and signed off by our own lab.

Four induction furnaces melt carbon, low-alloy and stainless grades from sorted scrap and virgin alloys. Every heat is sampled on the spectrometer before the ladle leaves the furnace, so a chemistry miss is corrected in the melt, not found on the part.

Patterns are made in-house in wood, polystyrene or 3D-printed resin, and customer patterns are stored free of charge for five years.
Pour weight50 kg – 12 t
Furnaces4 × induction, 2–6 t
GradesCarbon, low-alloy, stainless, Ni-hard
MouldingFuran sand, investment
StandardEN 10293 / ASTM A27
CertificatesEN 10204 3.1 / 3.2

Chemistry before pouring

A spectrometer check on every heat before the ladle leaves the furnace.

Simulated moulds

Solidification is simulated before pattern making to design out porosity.

Re-pour, not repair

We re-pour instead of repair welding unless you approve otherwise in writing.

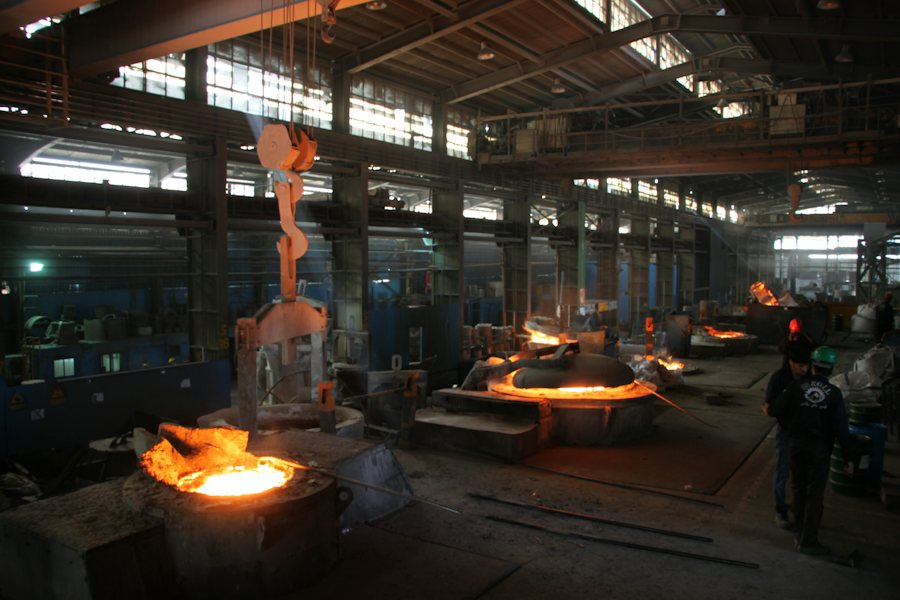
Glowing furnaces on a foundry floor
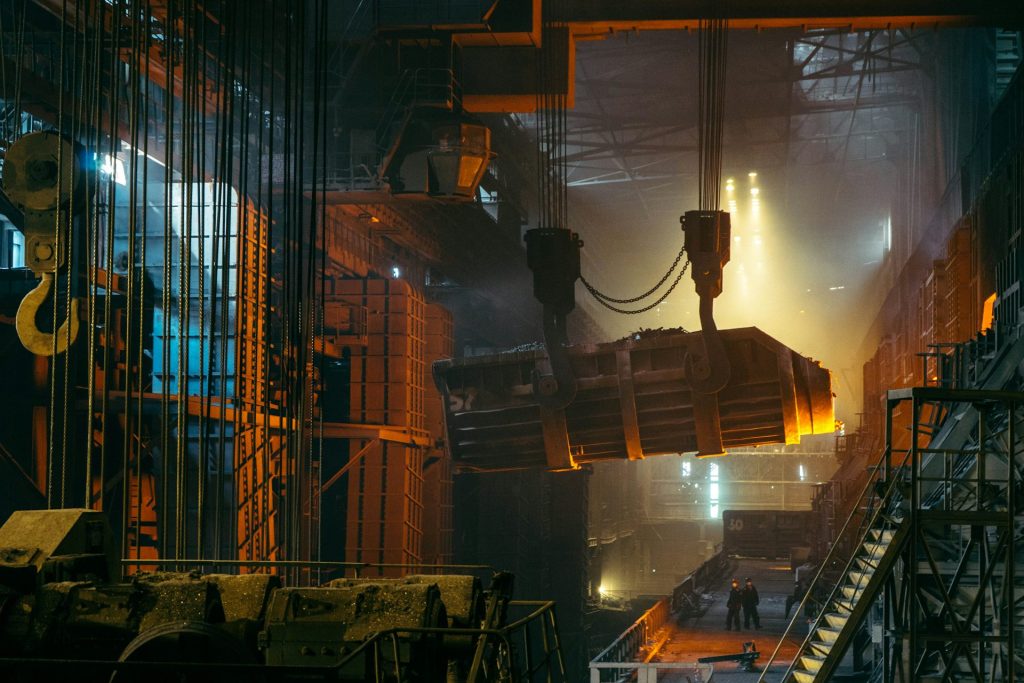
Crane lifting a glowing ladle in the melt shop

Questions about melting and casting

One piece, if the pattern exists. For new patterns we usually recommend a run of five or more to spread the tooling cost.

Yes. We make wooden, polystyrene and 3D-printed patterns in-house and store customer patterns free of charge for five years.

Usually. Send the chemistry and mechanical requirements and a metallurgist confirms within two working days.

Next service

Open-die forging

Shafts, rings and blocks up to 18 t on a 2,500 t press, with the reduction ratio recorded for every piece.
Buy Theme - $49 Launch It For Me