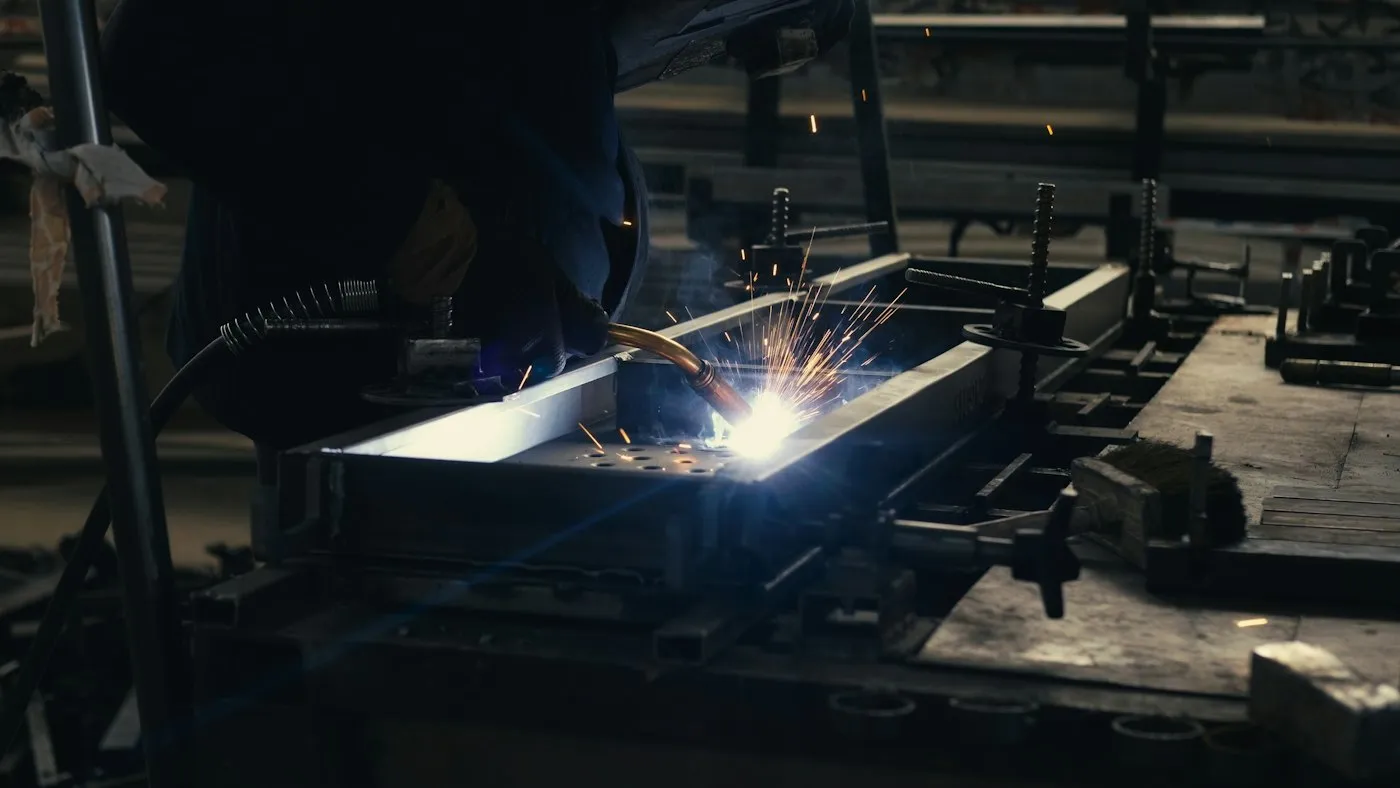
Machine bases move. A welded steel frame carries the stress of every weld in it, and the moment you machine one face flat, the frame relaxes and the face is no longer flat. Every fabricator knows this. Fewer measure it.
Last month we built a 4-metre base for a grinding machine and measured it at three points in its life: as welded, after stress relief, and after machining. Here are the numbers.
As welded
Flatness of the top face across the full 4 m length, measured on the CMM with the frame supported at its three mounting points: 3.8 mm. Twist corner to corner: 2.1 mm. Not unusual for forty metres of weld.
After stress relief
The base went into the furnace at 580 °C for four hours and cooled overnight with the furnace. Flatness the next morning: 4.6 mm. Twist: 2.4 mm. It got worse, which is the whole point: the stress the welds had locked in has now come out, and it came out as movement. Better in the furnace than on the customer’s floor.
A frame that moves in the furnace is a frame that will not move in service. The one to worry about is the one that does not.
After machining
Top face milled in one pass on the 5-axis, base mounted the way it will be mounted on site. Flatness: 0.04 mm across 4 m. Twist: 0.03 mm. Measured again three weeks later, after the base had sat in the hall: no change.
Why the order matters
Skip the furnace and machine the frame straight from the welding jig and you will hit 0.04 mm too. It will read 0.4 mm a month later. Stress relief is not a finishing step; it is the step that makes finishing mean anything.